

Profile and cooling-hole inspection of turbine blades
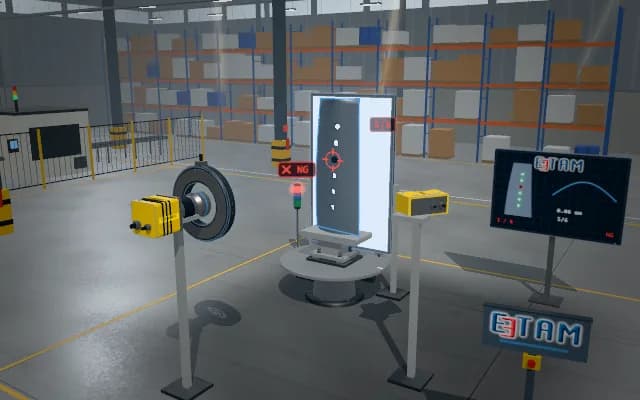
As a turbine blade is indexed in a rotary fixture, a laser profiler measures its surface sections. A facing telecentric camera checks the cooling holes with light from behind; a hole that passes no light is shown with a red ring and the blade is set aside for review.
Section deviation and the hole status map are added to the blade record; the position of a blocked hole is shown on the operator display and the blade is set aside for maintenance review.
- 01 Fixture
- 02 Index
- 03 Scan
- 04 Compare
- 05 Review
The blade is clamped by its root in the rotary fixture.
- Profile deviation
- —
- Open holes
- —
- Blocked holes
- —
Scenes are illustrative simulations; they are not customer references or performance guarantees.
Need
The curved metal blade changes its glare with viewing direction. Small holes and dark reflection patches can look alike; profile and hole inspection require different lighting geometries.
Solution approach
The rotary fixture presents the blade to the profiler at different angles; sections are compared with the nominal blade form. A telecentric camera faces the hole row squarely with the backlight directly behind: an open hole appears bright, a blocked hole dark. A ring light brings out hole edges and positions.
Process steps
- 01
Fixture
The blade is clamped by its root in the rotary fixture.
- 02
Index
The fixture indexes the blade to the scanning angles.
- 03
Scan
Laser sections and the hole image are acquired.
- 04
Compare
Profile and hole map are compared with the reference.
- 05
Review
The location of a blocked hole is marked.
Related applications



Let us assess your application together
We test your sample in our laboratory and report on resolution, optics and lighting selection.