

Cell polarity and arrangement verification in battery modules
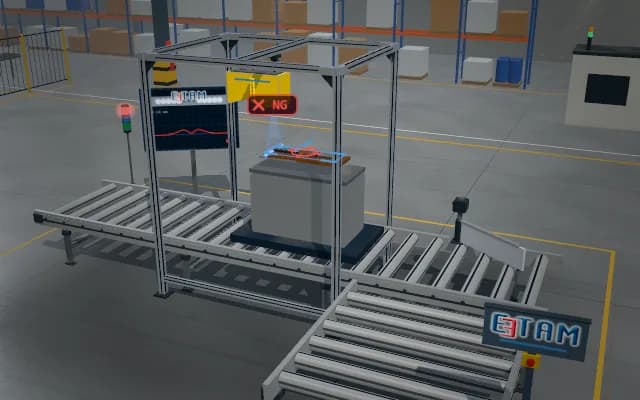
Before busbar welding, the cell carrier rests against a stop gate under the gantry; an overhead camera images the cell heads under a ring light. The protruding ring of the positive pole and the flat face of the negative pole are compared with the recipe pattern; a carrier with a reversed cell is not released to welding and is sent back for correction.
Expected and observed polarity matrices go to the operator display; a non-conforming slot is written to the module record. The PLC does not release busbar welding: the stop gate stays closed and the carrier is sent back to the loading side for correction.

- 01 Positioning
- 02 Acquire
- 03 Analyse
- 04 Decide
The cell carrier rests against the stop gate under the gantry before welding.
- Observed cells
- —
- Pole mismatch
- —
Scenes are illustrative simulations; they are not customer references or performance guarantees.
Need
Metal reflections from adjacent cell heads can obscure pole shapes. Missing cells, reversed poles or differing types must be distinguished slot by slot before busbar welding.
Solution approach
The gantry camera looks straight down at the cell heads; the ring light around it renders the protruding ring of the positive pole as a distinct ring and the negative pole as a flat disc. The two are separated by shape; cell presence, the pole matrix and visible codes are compared with the recipe slots.
Process steps
- 01
Positioning
The cell carrier rests against the stop gate under the gantry before welding.
- 02
Acquire
Cell heads and codes are imaged under the ring light.
- 03
Analyse
The observed pole matrix is compared with the recipe arrangement.
- 04
Decide
The reversed cell is marked; the carrier is not released to welding and is sent back.
Related applications




Let us assess your application together
We test your sample in our laboratory and report on resolution, optics and lighting selection.