

Dent and waviness profile on cable jackets
The cable passes through circumferential profile heads at the extrusion outlet. Outer-jacket sections are compared with the nominal shape; the length positions of local dents and waviness are entered in the winding record.
Depression and waviness profiles go to the operator display; defective lengths are flagged in the winding record and region data is sent to the line PLC.
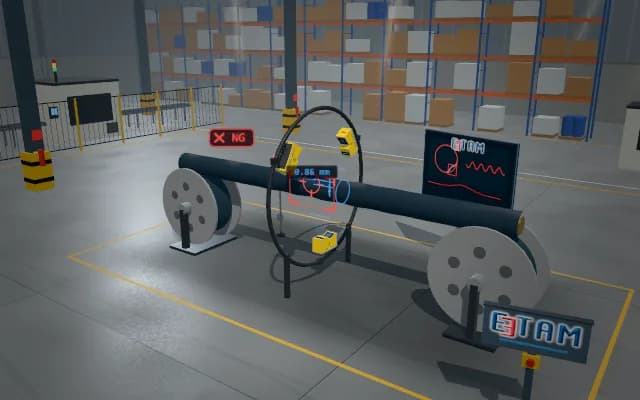
- 01 Extrusion outlet
- 02 Circumferential scan
- 03 Section matching
- 04 Shape deviation
- 05 Winding record
The cable travels between guides.
- Dent depth
- —
- Waviness
- —
Scenes are illustrative simulations; they are not customer references or performance guarantees.
Need
The rear of a cylindrical jacket is hidden from a single sensor. Weak reflection from a dark surface and cable sway can confuse actual dents with position changes.
Solution approach
Laser profile heads around the cable view the outer section from different angles. Profiles are transformed to a common axis and compared with the nominal circumference; successive sections reveal local depression and longitudinal waviness.
Process steps
- 01
Extrusion outlet
The cable travels between guides.
- 02
Circumferential scan
Profile heads scan different sides.
- 03
Section matching
Sections are matched to a common cable axis.
- 04
Shape deviation
Dent and waviness are extracted against the nominal circumference.
- 05
Winding record
The defective length is reported to line control.
Related applications


Let us assess your application together
We test your sample in our laboratory and report on resolution, optics and lighting selection.