

Headlamp lens surface analysis and optical defect detection
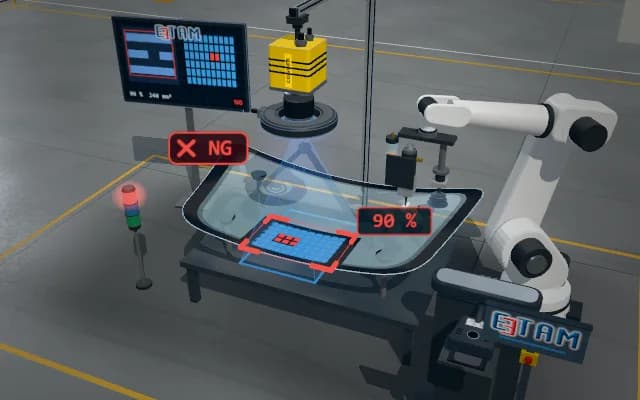
The headlamp is scanned on a rotary fixture under two lighting set-ups. Under low-angle dark-field light, scratches, bubbles and inclusions light up; the reflection of a stripe pattern in the lens exposes optical distortion as a local bend.
Surface defect count and optical deviation are sent to the operator display in the same part record. The combined NG decision is reported through the stack light and separation interface.

- 01 Index
- 02 Dark field
- 03 Stripe light
- 04 Distortion
- 05 Decide
The rotary fixture turns the next headlamp to face the camera.
- Surface defects
- —
- Largest defect
- —
- Stripe deviation
- —
Scenes are illustrative simulations; they are not customer references or performance guarantees.
Need
A curved headlamp lens is both transparent and reflective, so the camera sees the reflector and projector behind it along with the surface. Because the lens curvature already bends the stripe pattern, a local optical distortion has to be separated from this geometric bending.
Solution approach
The rotary fixture turns the headlamp to face the camera. Low-angle bar lights at the sides come on first: the smooth surface stays dark, while scratches and bubbles scatter light into the camera. The stripe panel reflected in the lens is then imaged as the pattern is shifted step by step; local stripe deviation reveals optical distortion. Both acquisitions are evaluated separately and combined.
Process steps
- 01
Index
The rotary fixture turns the next headlamp to face the camera.
- 02
Dark field
Under low-angle light, surface defects appear as bright dots and lines.
- 03
Stripe light
The stripe pattern reflects in the lens and is shifted step by step.
- 04
Distortion
Local deviation of the reflected stripes is measured.
- 05
Decide
Surface and optical results are combined.
Related applications






Let us assess your application together
We test your sample in our laboratory and report on resolution, optics and lighting selection.