

Surface defect inspection on MDF and particleboard
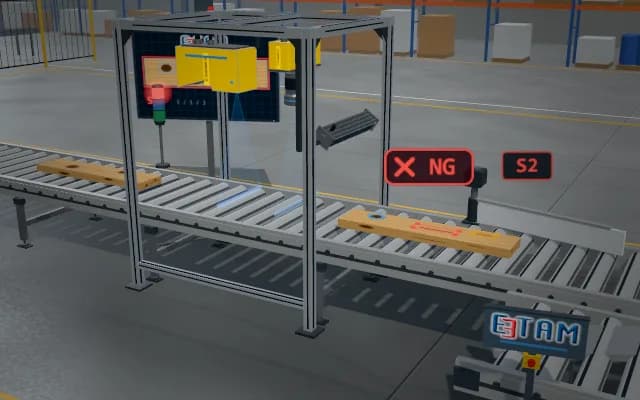
Leaving the press, the panel passes under a gantry on the roller conveyor; two line-scan cameras mounted across the panel scan the surface under two lighting geometries. Bright-field reveals stains and paper tears, low-angle light reveals blisters and dents; defects are logged on the panel map and the panel is routed to the stacker by quality grade.
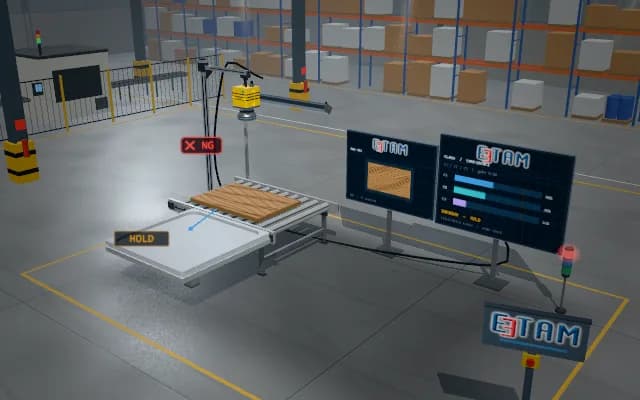
The panel map and defect list are written to the quality record; the grade code goes to the stacker PLC and the panel is routed to the first or second grade stack.

- 01 Infeed
- 02 Scan
- 03 Map
- 04 Decide
The panel from the press arrives at the gantry on the roller conveyor.
- Defects
- —
- Largest defect
- —
- Grade
- —
Scenes are illustrative simulations; they are not customer references or performance guarantees.
Need
The panel is wide and moves fast; the height of a blister or dent is small and invisible under steep light, while a stain disappears under low-angle light. The natural pattern of the melamine film and the chip texture of a raw board blend with the defects.
Solution approach
Two line-scan cameras side by side cover the full panel width; encoder-triggered scanning gives constant sampling regardless of speed. The bright-field image under a steep bar light shows dark stains and paper tears; the image under a second, very low-angle bar light shows the shadow-highlight pair of blisters and dents. Both images are merged in panel coordinates and graded by defect size.
Process steps
- 01
Infeed
The panel from the press arrives at the gantry on the roller conveyor.
- 02
Scan
Two line-scan cameras read the surface line by line under bright-field and low-angle light.
- 03
Map
Stains, blisters and scratches are logged on the panel map with their position.
- 04
Decide
Defect size and count are applied to the grade rule; the panel is routed to the corresponding stack.
Related applications


Let us assess your application together
We test your sample in our laboratory and report on resolution, optics and lighting selection.