

Coating uniformity and pinhole inspection on coated flat glass
At the coating-line exit, a glass sheet is scanned by line cameras in transmitted and reflected light. Bright pinholes and coating-tone variations across the width are mapped; defect regions are marked in the cutting plan.
The defect map in sheet coordinates and colour profile are sent to the cutting plan. A non-conforming region is marked on the display; the sheet is recorded for reassessment.
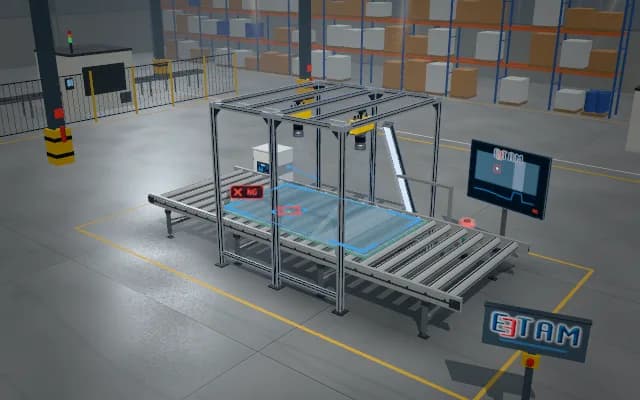
- 01 Position
- 02 Acquire
- 03 Analyse
- 04 Decide
The glass sheet enters the roller inspection area from the coating line.
- Pinhole count
- —
- Illustrative colour difference
- —
Scenes are illustrative simulations; they are not customer references or performance guarantees.
Need
Thin coatings appear different in colour with reflection angle; rollers and ambient light affect uniformity. Small pinholes may disappear in reflection but become distinct in transmitted light.
Solution approach
The first line camera scans coating openings as bright spots using a lower backlight bar. A second colour line camera images reflection under oblique top light; the colour profile across the width is compared with a reference. Both maps are combined in sheet coordinates.
Process steps
- 01
Position
The glass sheet enters the roller inspection area from the coating line.
- 02
Acquire
Transmitted-light and reflection images are acquired by separate line cameras.
- 03
Analyse
Bright spots and tone deviation across the width are mapped.
- 04
Decide
Defect positions are stored in the cutting plan and marked on the display.
Related applications



Let us assess your application together
We test your sample in our laboratory and report on resolution, optics and lighting selection.