

Flatness measurement of board before die-cutting
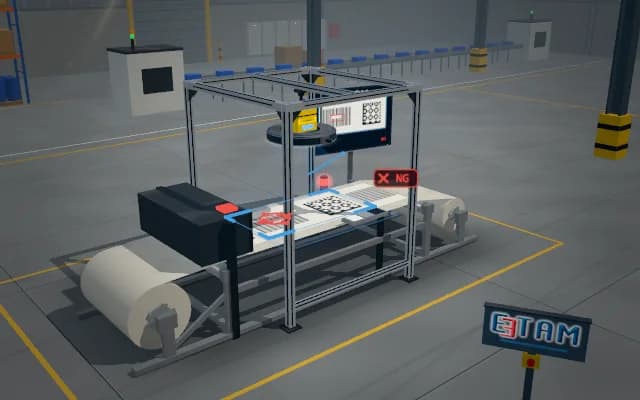
The board sheet is scanned from above with a laser profile as it moves from the feed table to the cutting unit. Curl and peak height deviation from the reference plane are calculated; an out-of-limit sheet is transferred to a side stack before cutting.
The height map and peak deviation go to the operator display; the PLC transfers an out-of-limit sheet to the side stack before cutting.

- 01 Positioning
- 02 Acquire
- 03 Analyse
- 04 Decide
The board sheet arrives from the feed table on the inspection belt.
- Peak deviation
- —
- Transverse curl
- —
Scenes are illustrative simulations; they are not customer references or performance guarantees.
Need
Moisture and transport stress can curl the board sheet. Position changes or sheet tilt on the belt can make local corner lift and plane deviation difficult to distinguish.
Solution approach
A gantry-mounted laser profile sensor scans across the sheet. A height map is formed from successive sections; the transport-plane reference is subtracted to evaluate peak deviation, edge waviness and corner lift.
Process steps
- 01
Positioning
The board sheet arrives from the feed table on the inspection belt.
- 02
Acquire
The laser line collects transverse sheet sections.
- 03
Analyse
Peak deviation from the plane is extracted from the height map.
- 04
Decide
The curled sheet is transferred to a side stack before cutting.
Related applications



Let us assess your application together
We test your sample in our laboratory and report on resolution, optics and lighting selection.