

Pull-tab inspection on beverage cans
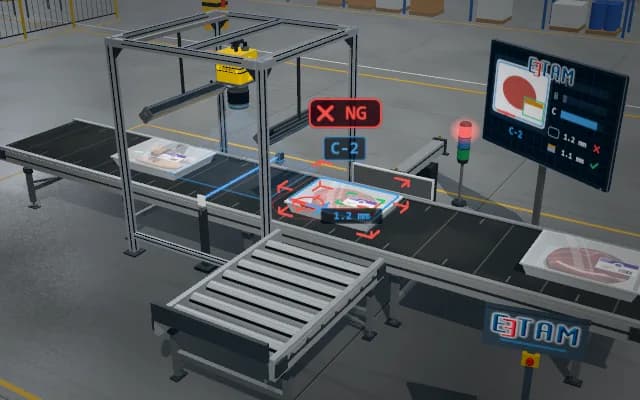
The can lid is scanned by laser profiling after closing. Pull-tab height and plane are measured relative to the lid reference; a raised, crushed or missing tab is removed from the line.
Tab height and tilt are sent to the PLC; an out-of-limit can is separated by the pusher. The lid map and decision are shown on the operator display.

- 01 Infeed
- 02 Trigger
- 03 Acquire
- 04 Analyse
- 05 Decision and separation
The product is carried into the inspection station.
- Tab height
- —
- Tab tilt
- —
Scenes are illustrative simulations; they are not customer references or performance guarantees.
Need
Reflections and embossing on the shiny lid can resemble pull-tab edges. A flat top-view image does not reveal the height of a tab lifted away from the lid.
Solution approach
A laser profile sensor on the gantry acquires cross-sections across the belt. The lid plane is used as a reference to calculate tab height and tilt. The out-of-limit tab region is marked on the height map.
Process steps
- 01
Infeed
The product is carried into the inspection station.
- 02
Trigger
The photo-sensor reports the product position.
- 03
Acquire
The lid is scanned with laser sections across the belt.
- 04
Analyse
The tab plane is measured relative to the lid reference.
- 05
Decision and separation
The result is sent to the display and PLC; a non-conforming product is separated.
Related applications




Let us assess your application together
We test your sample in our laboratory and report on resolution, optics and lighting selection.